
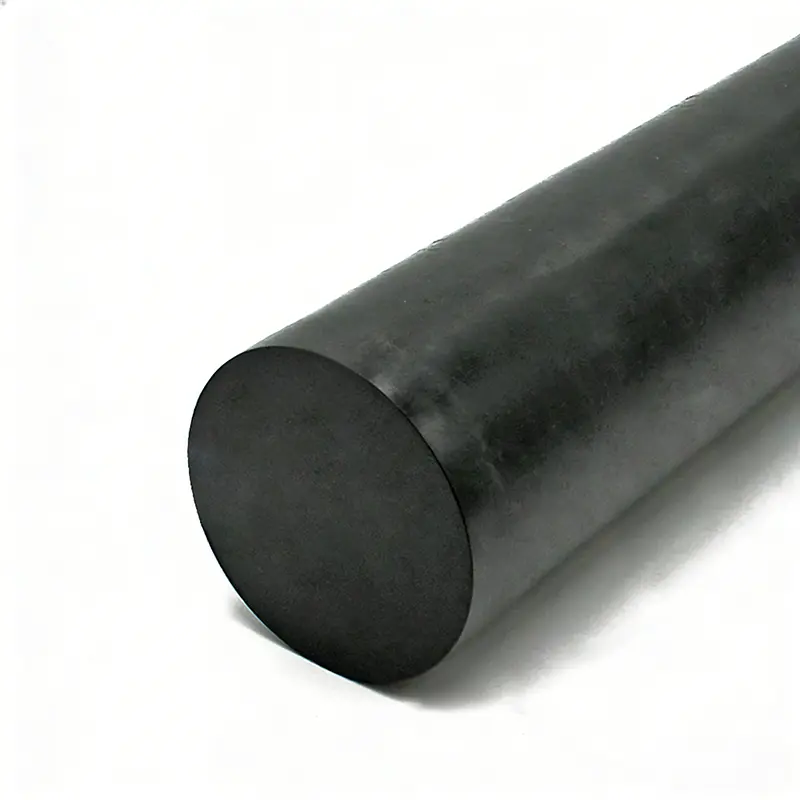
Glass-Filled PSU/PPSU Rods & Sheets
High Flexural Modulus | HDT up to 210°C | Metal-Replacement Stock Shapes
Supplied as high-density structural machining stock, our Glass-Filled PSU & PPSU Rods & Sheets (GF20%–30%) are engineered for heavy-duty fluidic manifolds, valve bodies, and medical trays requiring elevated stiffness and dimensional retention under load. Formulated to match data sheets for Tecason® GF30 series, our glass-reinforced stock shapes elevate Heat Deflection Temperature up to 210°C (GF-PPSU) / 180°C (GF-PSU) and replace heavy brass, aluminum, and stainless steel in hot fluid systems.
Send your target sheet thickness, rod diameter, or drawing below for an immediate factory quote.
Product information
Published information supports preliminary product selection. Confirm the exact grade, dimensions, tolerances, documentation and application suitability with the quotation for your order.
Description
Practical Material Behavior: Why Specify Glass Fiber Fillers?
While unfilled PSU and PPSU resins offer high toughness and optical transparency, their flexural modulus (~2,400 MPa) can flex under continuous heavy mechanical loads.
Adding 20% to 30% glass fibers doubles or triples the flexural modulus (up to 7,500+ MPa), reduces the Coefficient of Linear Thermal Expansion (CLTE), and dramatically improves compressive creep resistance under bolt clamping pressure.
GF-PSU vs. GF-PPSU Selection Guide
-
Specify Glass-Filled PSU (GF-PSU): When components require high stiffness, dimensional stability up to 160°C continuous (HDT ~180°C), and chemical resistance to hot mineral acids at an optimal material cost.
-
Specify Glass-Filled PPSU (GF-PPSU): When parts demand high structural modulus, 180°C continuous heat (HDT ~210°C), and resistance to 1,000+ steam autoclave sterilization cycles (134°C).
Machining Reality & Tooling Wear
Extruded and molded thick plates and round rods undergo a 72-hour thermal stress-relieving process to prevent plate bowing during 70%+ volume CNC milling.
Tooling Note: Glass fibers are highly abrasive to cutters. Carbide or PCD diamond CNC tools are mandatory to prevent rapid cutter dulling and ensure clean, burr-free thread profiles.
Material Boundaries (Engineering Drawbacks / 弊端)
-
⚠️ Loss of Transparency: Glass fiber fillers render the stock shape opaque beige/grey (complete loss of amber optical clarity).
-
⚠️ Reduced Impact Strength vs. Unfilled PPSU: Fiber reinforcement increases flexural rigidity, but reduces Izod impact toughness compared to 100% unfilled pure PPSU.
-
⚠️ Polar Organic Solvent Restriction: Like all amorphous sulfones, glass-filled PSU and PPSU are sensitive to Ketones (Acetone, MEK) and Esters, which cause Environmental Stress Cracking (ESC). (Select crystalline PPS or PEEK for ketone/ester exposure).
Quote Parameters & Ordering Checklist
Please provide:
-
Material Grade: Glass-Filled PSU (GF-PSU) or Glass-Filled PPSU (GF-PPSU).
-
Reinforcement Ratio: GF20% or GF30%.
-
Stock Form & Size: Sheet Thickness (5mm to 100mm+) × W × L or Rod Diameter (10mm to 150mm+).
-
Quantity: Number of sheets, rods, or cut-to-size pieces.
Material overview
Understanding PPS (Polyphenylene Sulfide)
Why engineers use it
- Broad chemical resistance for many industrial fluids and process environments.
- Low moisture uptake and good dimensional stability.
- Useful electrical insulation and inherent flame-resistance characteristics.
- Reinforced grades can provide high stiffness and repeatable molded dimensions.
- Often offers a practical cost/performance position below PEEK.
Limits to consider
- Unfilled PPS can be relatively brittle and design details strongly affect impact performance.
- Glass or mineral reinforcement changes shrinkage, anisotropy and machining behavior.
- Oxidizing media and actual high-temperature chemicals still require compatibility review.
- Weld lines, sharp corners and molding orientation can become structural weak points.
- It should not be selected from chemical-resistance charts alone.
Grades and product forms
PPS is commonly supplied unfilled or reinforced with glass fiber, mineral filler, carbon fiber or combined systems. The filler package changes stiffness, movement, surface finish, conductivity and wear. Pellets suit volume molding, while sheet, rod or finished parts may be preferable for prototypes and lower-volume production.
Performance points to review
| Evaluation area | Why it matters | Information to provide |
|---|---|---|
| Temperature behavior | Useful performance under elevated or changing temperature | Continuous and peak temperature, cycle length and time at load |
| Mechanical response | Strength and stiffness must match the real part geometry | Load direction, stress level, impact and fatigue expectations |
| Environmental resistance | Fluids, cleaning agents and atmosphere can change service life | Chemical name, concentration, temperature and exposure time |
| Dimensional control | Tight-tolerance parts depend on both material and processing | Finished dimensions, tolerances and assembly conditions |
| Electrical or insulation needs | Electrical requirements may influence grade and thickness | Voltage, dielectric, conductivity or insulation target |
These are engineering discussion points, not guaranteed property values. Final acceptance criteria should be agreed for the selected grade, process and order.
Typical application directions
These examples show where the material may be evaluated. They do not replace a suitability review for the finished component.
Fabrication and processing preparation
Share the finished part drawing as well as the requested rod diameter and length. This makes it possible to discuss machining allowance, tolerance, cut length, quantity and whether a closer starting size could reduce waste.
Where the application is critical, define what a successful trial looks like before material is ordered: dimensions after processing, visual condition, mechanical response, assembly fit or another measurable result.
When another material may be better
PEEK may be preferred when toughness or a broader high-temperature performance margin is required. PPS can be the more practical solution when chemical resistance, stiffness, repeatable molding and cost control are the central requirements.
We recommend sharing the current material and the reason it is being reconsidered. Cost, processability, supply form and inspection burden belong in the decision alongside technical performance.
Information needed for an accurate quotation
A useful RFQ reduces follow-up questions and helps us distinguish between a material request and a finished-part requirement.
| Product form | Raw material, stock shape, semi-finished blank or completed part |
|---|---|
| Dimensions | Nominal size, finished size and tolerances |
| Quantity | Trial quantity, first order and estimated annual demand |
| Application | Part function and current material, if any |
| Operating temperature | Continuous range, peak temperature and cycle duration |
| Environment | Chemicals, gases, moisture, pressure, vacuum or outdoor exposure |
| Mechanical duty | Load, speed, impact, wear and mating components |
| Documentation | Drawing revision, inspection, traceability or compliance needs |
Frequently asked questions
Can I request a sample or trial quantity?
Trial quantities can be discussed according to product form and availability. Tell us what you need to prove during the trial, the intended process and the expected production quantity if the test succeeds.
Do you provide a data sheet or material documentation?
Available documentation depends on the selected material and supply route. List the documents required by engineering, purchasing or quality when you inquire so they can be checked before quotation.
Can the grade be selected from a product name alone?
No. Similar product names can cover different grades, colors, fillers and processes. Selection should be based on the finished application, environment and required property balance.
Can you supply custom dimensions or finished parts?
Custom sizes, blanks or finished parts can be reviewed where appropriate. A drawing with tolerances, quantity and material requirement is the best basis for quotation.
How should we evaluate an alternative to our current material?
Share the current grade, the part’s service conditions and the reason for changing it. A useful comparison looks at failure mode, processing, life, inspection and total project cost—not only a single property value.
What determines lead time?
Lead time depends on product form, grade, size, quantity, documentation, machining and current availability. Confirm the required delivery date and destination with the RFQ rather than assuming a standard schedule.
Send the drawing, application and quantity. We will use the project details to prepare a practical material and supply discussion.
Reviews
There are no reviews yet.