
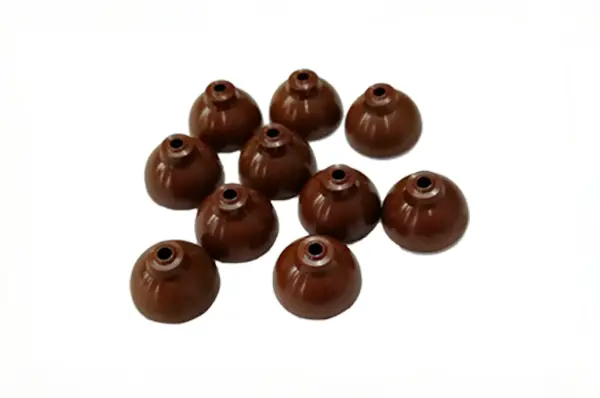
PI Thermal Insulation Cap
Stop thermal failures where PEEK and PTFE melt or creep.
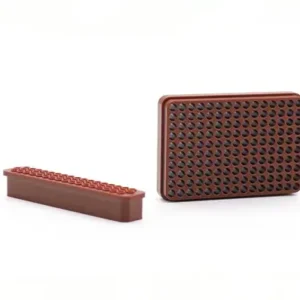
Engineered from pure Polyimide (PI), this insulation cap acts as an ultra-high temperature thermal choke and electrical barrier for extreme semiconductor, vacuum, and sensor environments.
• No Thermal Creep up to 300°C (400°C+ peak): Holds mechanical clamping force under continuous baking without softening or loosening fasteners.
• Zero Chamber Contamination: NASA-grade low outgassing and non-shedding—safe for plasma etching, CVD, and UHV systems.
• Precision Electrical Isolation: Dielectric barrier with ±0.01 mm tolerance for micro-fasteners and probes, 100% burr-free.
Direct CNC Manufacturer • Rapid Prototyping in 3–5 Days • Custom to Your STEP/CAD Drawings
Product information
Published information supports preliminary product selection. Confirm the exact grade, dimensions, tolerances, documentation and application suitability with the quotation for your order.
Description
Built to Replace Failing PEEK & PTFE in Critical Thermal Environments
When operating above 250°C in vacuum or plasma systems, standard plastics soften, creep, or outgas. Our precision-machined PI (Polyimide) Insulation Caps solve these real-world assembly failures directly:
4 Assembly Problems We Solve:
-
Fastener Loosening & Thermal Creep
Non-melting PI retains rigid clamping force at 300°C continuous (400°C+ peak). No bolt loosening, seal loss, or thermal collapse under heavy mechanical loads. -
Ceramic Cracking from Thermal Expansion
Low, controlled thermal expansion (matched to ceramics and metals) prevents excessive expansion stress, protecting delicate adjacent ceramic insulators during rapid thermal cycling. -
Vacuum Contamination & High-Temp Blistering
Ultra-low outgassing (CVCM < 0.1%) prevents wafer and optical lens contamination. Fully annealed and vacuum-packaged with desiccant to eliminate moisture-induced blistering under heat. -
Micro-Bore Burr Snagging & Misalignment
Tight CNC tolerance down to ±0.01 mm with true concentricity within 0.005 mm. 100% microscopically deburred—ensuring thermocouple probes and micro-screws slide in cleanly with zero friction.
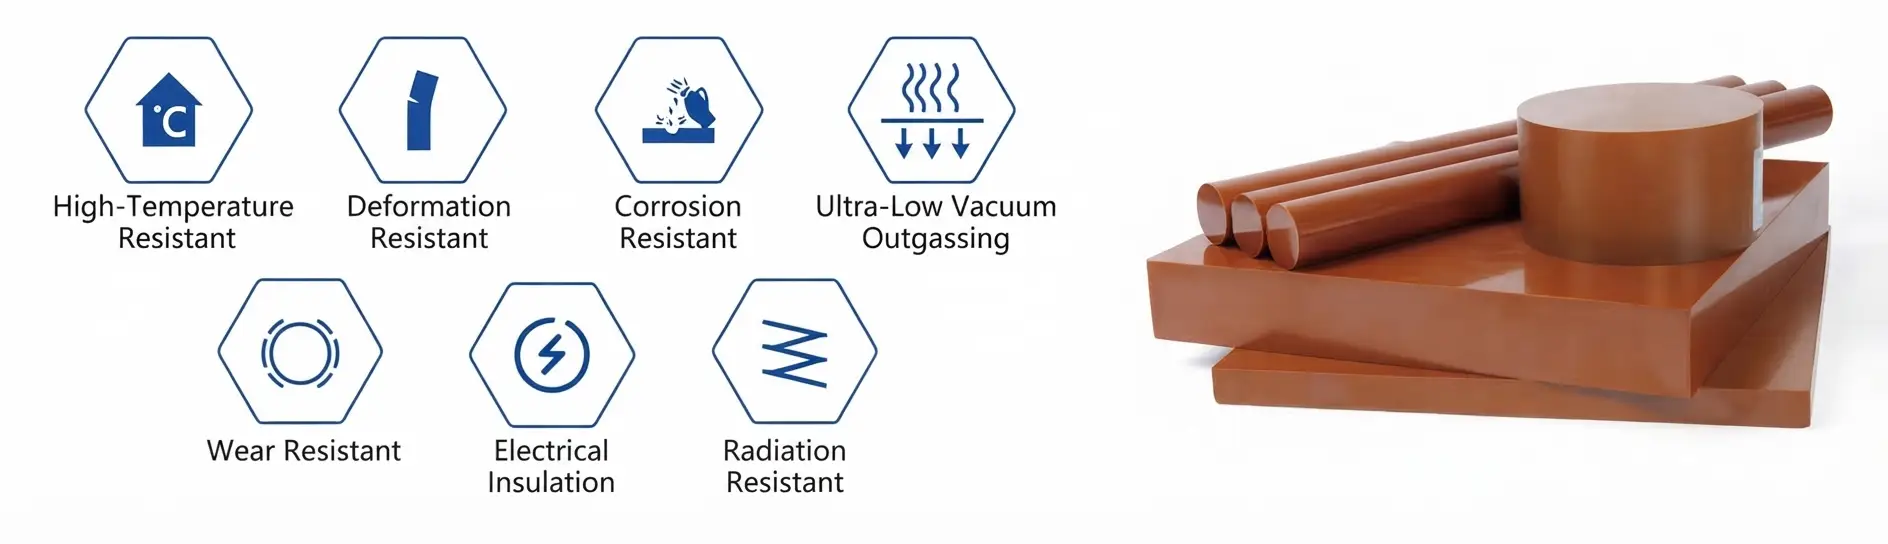
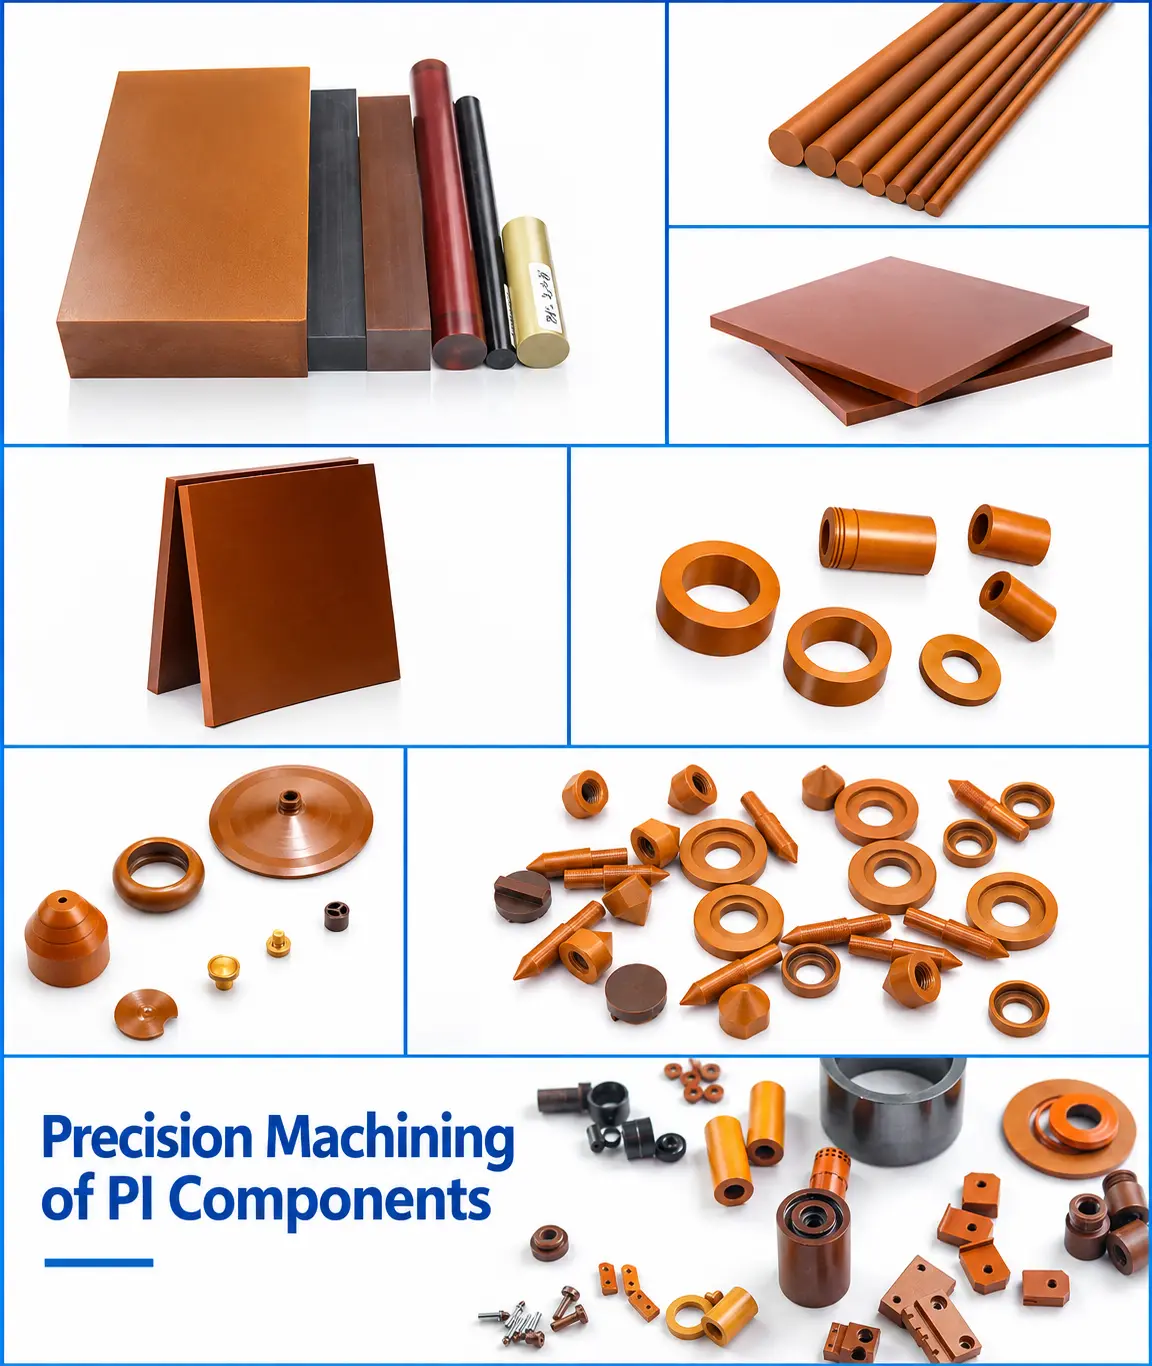
Applications of Ultra-High-Temperature Polyimide (PI) Polymers
Currently widely utilized across diverse industries, including automotive, semiconductors, office automation (OA) equipment, electrical & electronics (E&E), scientific instruments, hot runner systems, petrochemical equipment, industrial machinery, textile machinery, laser printing, and medical devices.
(1) Components operating under high-speed and high-pressure (high-PV) conditions requiring a low coefficient of friction (COF) and superior wear resistance;
(2) Precision components requiring outstanding resistance to creep and plastic deformation;
(3) Tribological parts demanding superior self-lubricating or oil-lubricated performance;
(4) Fluid and liquid sealing components under high-temperature and high-pressure (HTHP) environments;
(5) High-load mechanical components requiring exceptional flexural strength, tensile strength, and impact resistance;
(6) Critical components requiring high chemical corrosion resistance, radiation resistance, and zero rust/oxidation;
(7) Severe-service components with continuous operating temperatures exceeding 300°C, and short-term excursion capabilities up to 400–450°C;
(8) High-temperature structural adhesives for operating environments above 260°C (surpassing the temperature limits of modified epoxy, modified phenolic, and modified silicone adhesives, which typically fail below 260°C);
(9) Advanced semiconductor solutions: microelectronic packaging, stress-buffer protective coatings, interlayer dielectric (ILD) insulation for multilayer interconnect structures, high-performance dielectric films, and wafer/chip surface passivation layers.
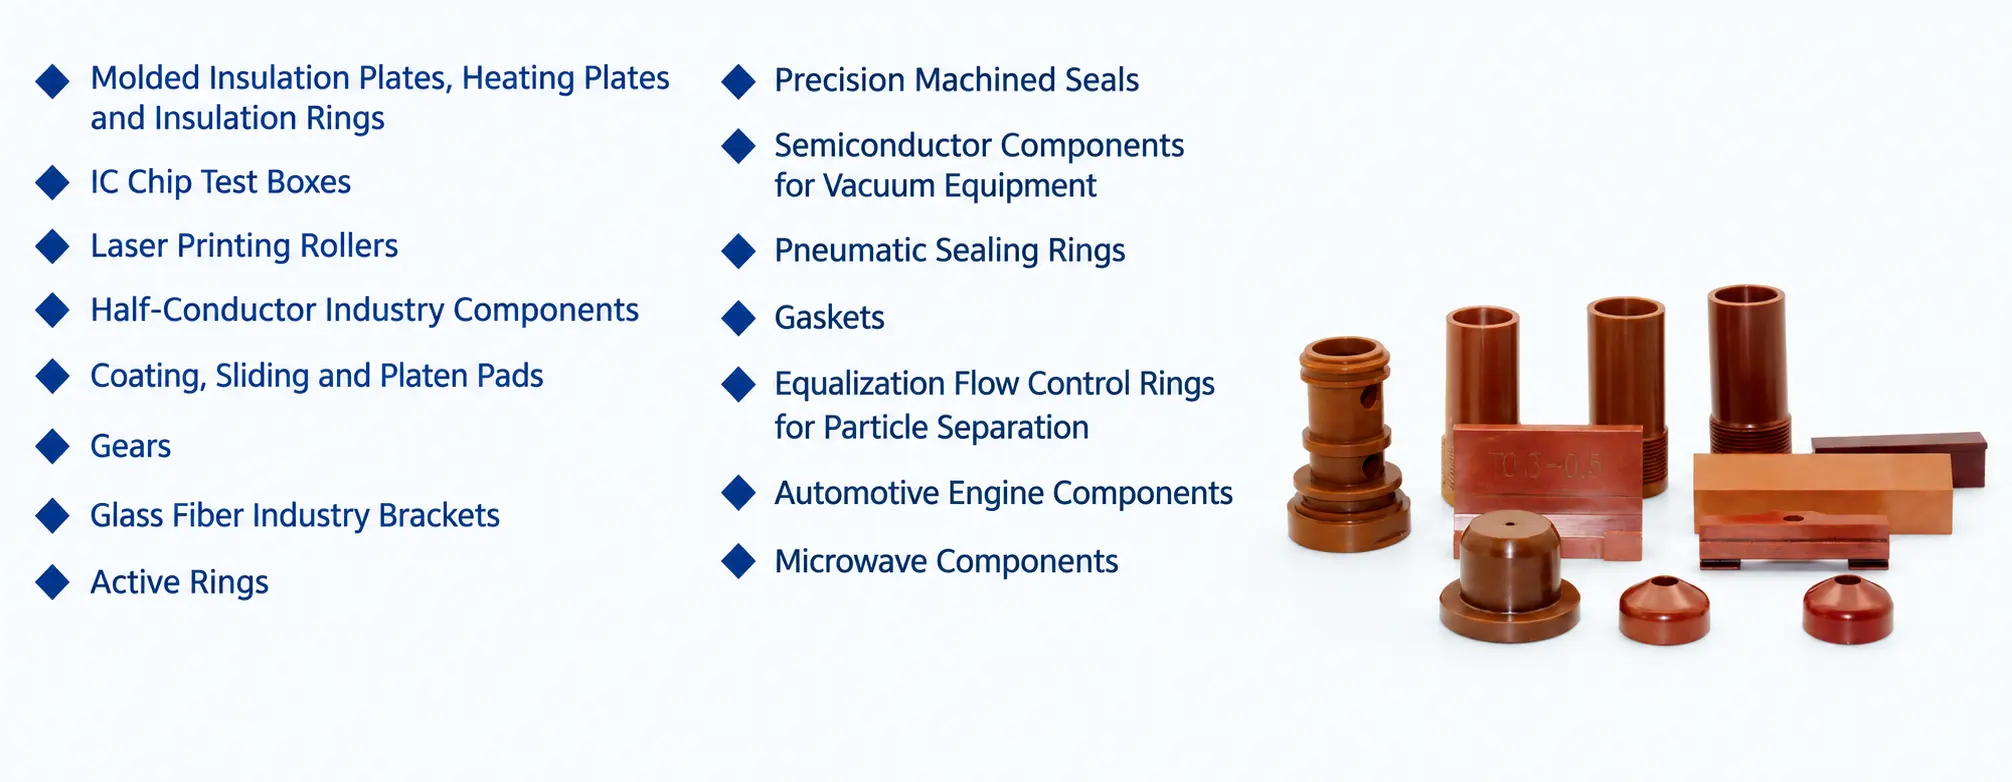
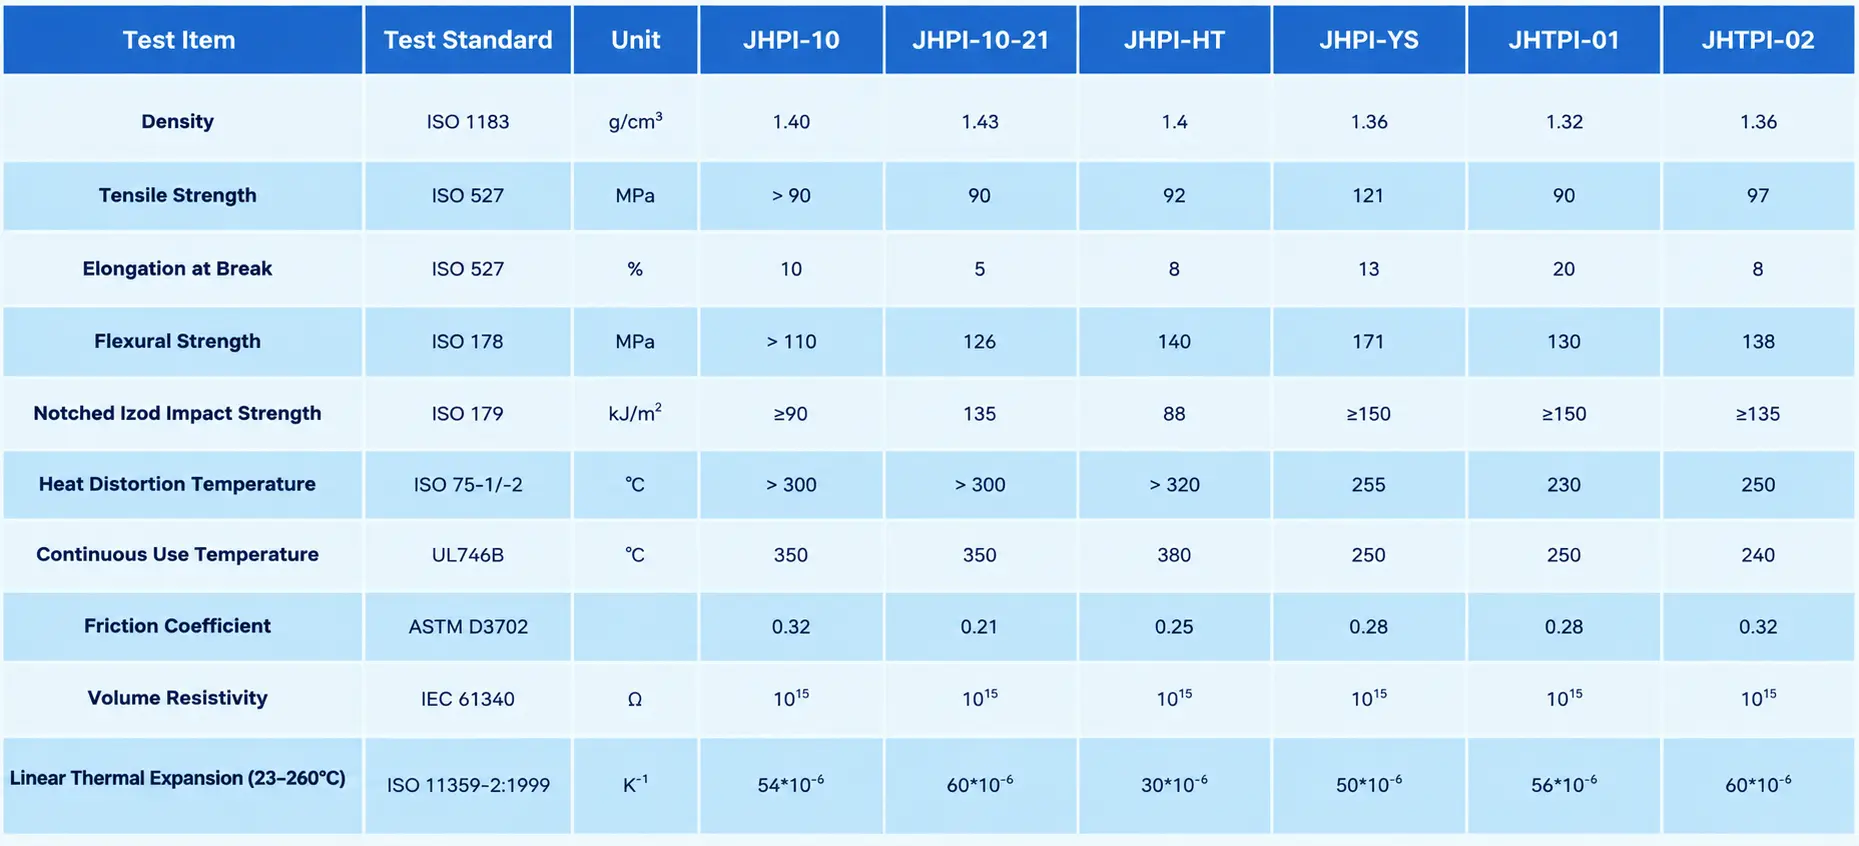
Performance Table of Ultra-High Temperature Polyimide (PI) Polymers
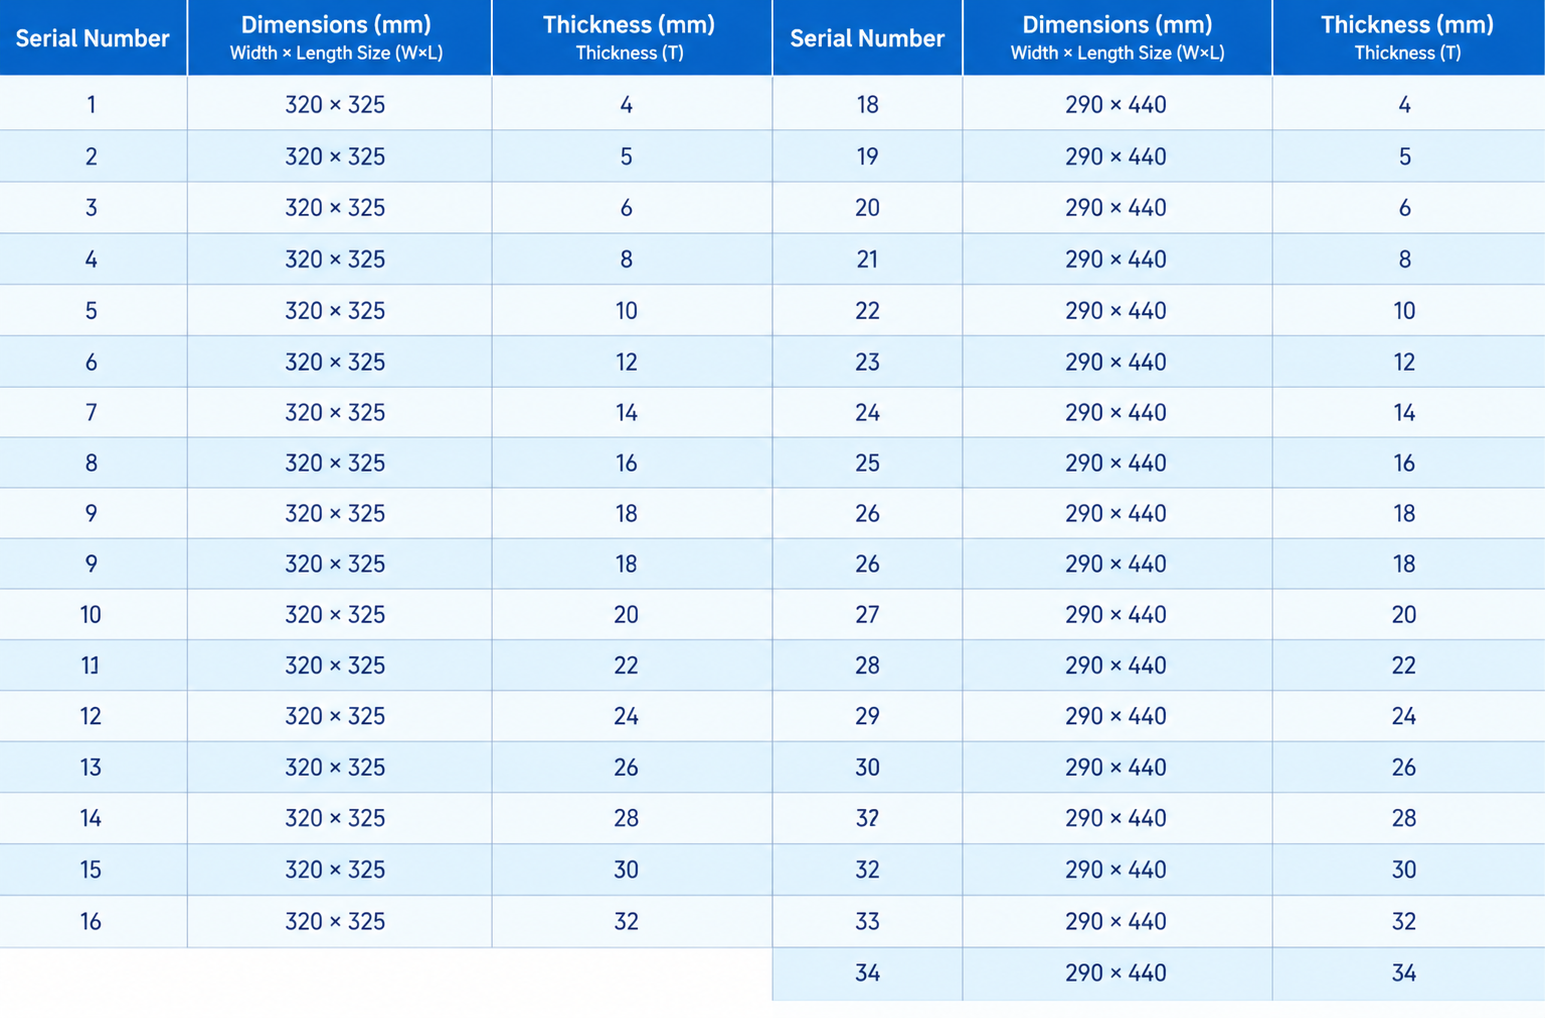
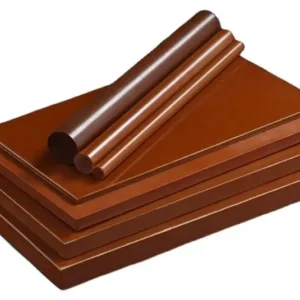
Ultra-High Temperature Polyimide (PI) Sheet and Rod Specifications
Material overview
Understanding PI (Polyimide)
Why engineers use it
- Strong thermal stability for electrical and mechanical applications.
- Excellent insulation potential in films and precision parts.
- Low wear and low outgassing options in selected grades.
- Good dimensional control in carefully processed components.
- Available in forms suited to insulation, machining or formulation work.
Limits to consider
- “PI” is a family name, not a single universal grade.
- Moisture, processing route and fillers affect dimensions and performance.
- Some forms cannot be melt processed like ordinary thermoplastics.
- High cost requires a clearly defined performance need.
- Acceptance values must be tied to the exact product and test method.
Grades and product forms
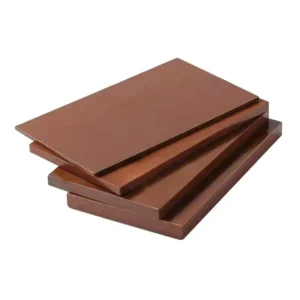
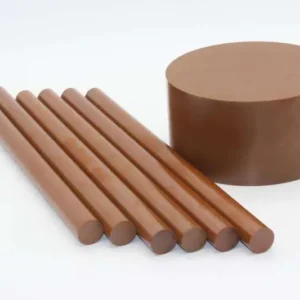
Film grades target flexible insulation; powder and resin support formulation or molding routes; stock shapes serve machined components; graphite, PTFE or other fillers may tune wear and friction. Product form and grade must be identified explicitly in the RFQ.
Performance points to review
| Evaluation area | Why it matters | Information to provide |
|---|---|---|
| Temperature behavior | Useful performance under elevated or changing temperature | Continuous and peak temperature, cycle length and time at load |
| Mechanical response | Strength and stiffness must match the real part geometry | Load direction, stress level, impact and fatigue expectations |
| Environmental resistance | Fluids, cleaning agents and atmosphere can change service life | Chemical name, concentration, temperature and exposure time |
| Dimensional control | Tight-tolerance parts depend on both material and processing | Finished dimensions, tolerances and assembly conditions |
| Electrical or insulation needs | Electrical requirements may influence grade and thickness | Voltage, dielectric, conductivity or insulation target |
These are engineering discussion points, not guaranteed property values. Final acceptance criteria should be agreed for the selected grade, process and order.
Typical application directions
These examples show where the material may be evaluated. They do not replace a suitability review for the finished component.
Fabrication and processing preparation
Confirm the intended manufacturing route, finished dimensions, critical tolerances and annual volume. A drawing allows the starting material and processing sequence to be discussed with fewer assumptions.
Where the application is critical, define what a successful trial looks like before material is ordered: dimensions after processing, visual condition, mechanical response, assembly fit or another measurable result.
When another material may be better
PBI and PAI can address different extremes of heat, strength and wear, while PEEK may offer easier processing for some applications. PI is selected when its thermal, electrical or tribological balance solves the specific design problem.
We recommend sharing the current material and the reason it is being reconsidered. Cost, processability, supply form and inspection burden belong in the decision alongside technical performance.
Information needed for an accurate quotation
A useful RFQ reduces follow-up questions and helps us distinguish between a material request and a finished-part requirement.
| Product form | Raw material, stock shape, semi-finished blank or completed part |
|---|---|
| Dimensions | Nominal size, finished size and tolerances |
| Quantity | Trial quantity, first order and estimated annual demand |
| Application | Part function and current material, if any |
| Operating temperature | Continuous range, peak temperature and cycle duration |
| Environment | Chemicals, gases, moisture, pressure, vacuum or outdoor exposure |
| Mechanical duty | Load, speed, impact, wear and mating components |
| Documentation | Drawing revision, inspection, traceability or compliance needs |
Frequently asked questions
Can I request a sample or trial quantity?
Trial quantities can be discussed according to product form and availability. Tell us what you need to prove during the trial, the intended process and the expected production quantity if the test succeeds.
Do you provide a data sheet or material documentation?
Available documentation depends on the selected material and supply route. List the documents required by engineering, purchasing or quality when you inquire so they can be checked before quotation.
Can the grade be selected from a product name alone?
No. Similar product names can cover different grades, colors, fillers and processes. Selection should be based on the finished application, environment and required property balance.
Can you supply custom dimensions or finished parts?
Custom sizes, blanks or finished parts can be reviewed where appropriate. A drawing with tolerances, quantity and material requirement is the best basis for quotation.
How should we evaluate an alternative to our current material?
Share the current grade, the part’s service conditions and the reason for changing it. A useful comparison looks at failure mode, processing, life, inspection and total project cost—not only a single property value.
What determines lead time?
Lead time depends on product form, grade, size, quantity, documentation, machining and current availability. Confirm the required delivery date and destination with the RFQ rather than assuming a standard schedule.
Send the drawing, application and quantity. We will use the project details to prepare a practical material and supply discussion.
Reviews
There are no reviews yet.