
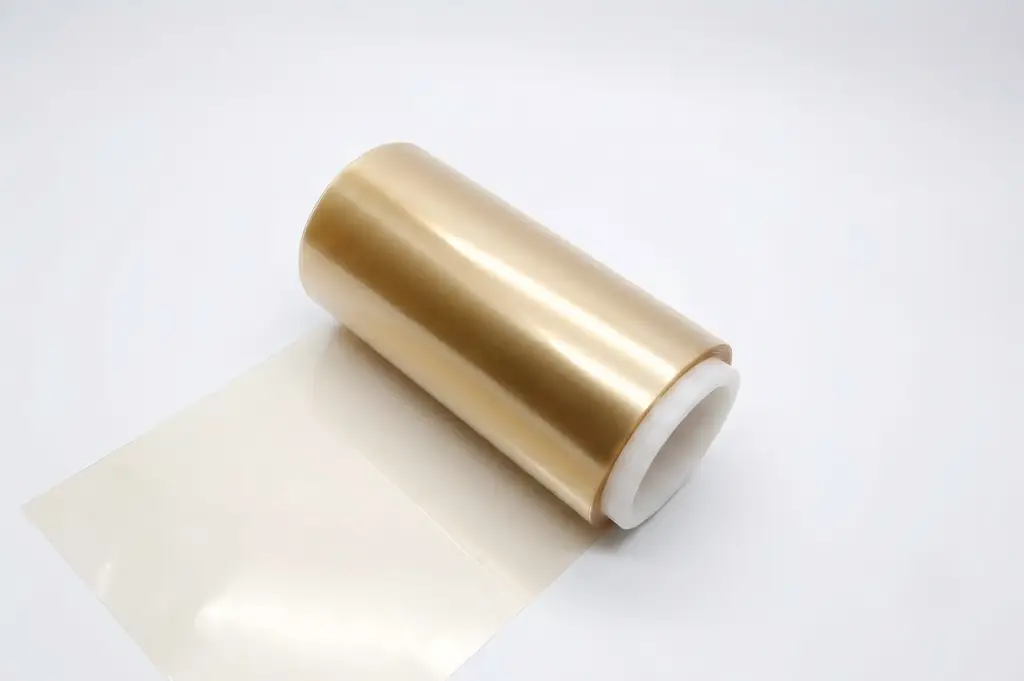
Autoclavable PPSU Film (0.025-0.5mm) | Steam Resistant
Engineered for extreme steam autoclaving and harsh chemical exposure, Vantpoly® DFPPSU Film features a 𝑇𝑔 of 220°C and continuous thermal stability at 180°C.With >110% ultimate elongation (super tough), 86.8% light transmittance, and 45 kV/mm dielectric strength, this halogen-free film is the preferred choice for hydrogen fuel cell gaskets, autoclavable medical wraps, and FDA-compliant food contact equipment.
Product information
Published information supports preliminary product selection. Confirm the exact grade, dimensions, tolerances, documentation and application suitability with the quotation for your order.
Description
Material Selection: PPSU vs. PEI vs. PEEK Film
| Performance Metric | PPSU Film (DFPPSU) | PEI Film (ULTEM™) | PEEK Film |
| Steam Autoclaving Resistance | Unlimited Cycles (Best) | Limited Cycles (Risk of crazing) | Excellent |
| Impact Toughness & Elongation | Extremely High (>110%) | Moderate (30% – 45%) | High |
| Glass Transition Temp (𝑇𝑔) | 220°C | 217°C | 143°C |
| Light Transmittance | 86.8% (Amber Clear) | 85.6% | Opaque / Translucent |
| Material Cost | Cost-Effective | Cost-Effective | Premium / High Cost |
Property Datasheet Summary (Grade DFPPSU)
| Parameter / Property | Technical Value |
| Thickness & Roll Width | 0.025–0.1mm (Width ≤ 950mm) / 0.1–0.5mm (Width ≤ 1050mm) |
| Surface Textures | Polished/Matte, Matte/Velvet |
| Tensile Yield Strength (MD/TD) | 68 MPa / 65 MPa |
| Elongation at Ultimate (MD/TD) | 125% / 117% (Super Tough) |
| Dielectric Strength / 𝐷ₖ | 45 kV/mm / 𝐷ₖ = 3.7 (1MHz) |
| Thermal Shrinkage (200℃/30min) | MD 0.5% / TD 0.2% |
Key Application Solutions
-
Hydrogen Fuel Cell Gaskets: Chemical-immune sealing gaskets for fuel cells and electrolyzers
-
Autoclavable Medical Devices: Medical wraps and trays resisting repeated steam sterilization
-
FDA Food & Beverage Equipment: Halogen-free, high-temp film for hot beverage seals and food contact
-
Automotive & EV Electronics: 45 kV/mm breakdown voltage for EV battery pack insulation and sensor windows
Frequently Asked Questions
Q: Why choose PPSU film instead of PEI (ULTEM™) film for medical devices?
A: PPSU film offers far superior steam autoclaving resistance and higher impact toughness (>110% elongation). While PEI film can micro-craze after repeated steam sterilization, PPSU film withstands unlimited autoclave cycles without degradation.
Q: Can PPSU film be thermoformed or heat-sealed?
A: Yes. DFPPSU film offers excellent thermoforming capability and heat-sealability for 3D protective covers and sealed pouches.
Material overview
Understanding PPS (Polyphenylene Sulfide)
Why engineers use it
- Broad chemical resistance for many industrial fluids and process environments.
- Low moisture uptake and good dimensional stability.
- Useful electrical insulation and inherent flame-resistance characteristics.
- Reinforced grades can provide high stiffness and repeatable molded dimensions.
- Often offers a practical cost/performance position below PEEK.
Limits to consider
- Unfilled PPS can be relatively brittle and design details strongly affect impact performance.
- Glass or mineral reinforcement changes shrinkage, anisotropy and machining behavior.
- Oxidizing media and actual high-temperature chemicals still require compatibility review.
- Weld lines, sharp corners and molding orientation can become structural weak points.
- It should not be selected from chemical-resistance charts alone.
Grades and product forms
PPS is commonly supplied unfilled or reinforced with glass fiber, mineral filler, carbon fiber or combined systems. The filler package changes stiffness, movement, surface finish, conductivity and wear. Pellets suit volume molding, while sheet, rod or finished parts may be preferable for prototypes and lower-volume production.
Performance points to review
| Evaluation area | Why it matters | Information to provide |
|---|---|---|
| Temperature behavior | Useful performance under elevated or changing temperature | Continuous and peak temperature, cycle length and time at load |
| Mechanical response | Strength and stiffness must match the real part geometry | Load direction, stress level, impact and fatigue expectations |
| Environmental resistance | Fluids, cleaning agents and atmosphere can change service life | Chemical name, concentration, temperature and exposure time |
| Dimensional control | Tight-tolerance parts depend on both material and processing | Finished dimensions, tolerances and assembly conditions |
| Electrical or insulation needs | Electrical requirements may influence grade and thickness | Voltage, dielectric, conductivity or insulation target |
These are engineering discussion points, not guaranteed property values. Final acceptance criteria should be agreed for the selected grade, process and order.
Typical application directions
These examples show where the material may be evaluated. They do not replace a suitability review for the finished component.
Preparing a high-temperature printing project
Provide filament diameter, printer model, nozzle and chamber capability, drying method, build geometry, support strategy and annealing plan. A high-performance filament cannot compensate for a printer that lacks the necessary thermal control.
Where the application is critical, define what a successful trial looks like before material is ordered: dimensions after processing, visual condition, mechanical response, assembly fit or another measurable result.
When another material may be better
PEEK may be preferred when toughness or a broader high-temperature performance margin is required. PPS can be the more practical solution when chemical resistance, stiffness, repeatable molding and cost control are the central requirements.
We recommend sharing the current material and the reason it is being reconsidered. Cost, processability, supply form and inspection burden belong in the decision alongside technical performance.
Information needed for an accurate quotation
A useful RFQ reduces follow-up questions and helps us distinguish between a material request and a finished-part requirement.
| Product form | Raw material, stock shape, semi-finished blank or completed part |
|---|---|
| Dimensions | Nominal size, finished size and tolerances |
| Quantity | Trial quantity, first order and estimated annual demand |
| Application | Part function and current material, if any |
| Operating temperature | Continuous range, peak temperature and cycle duration |
| Environment | Chemicals, gases, moisture, pressure, vacuum or outdoor exposure |
| Mechanical duty | Load, speed, impact, wear and mating components |
| Documentation | Drawing revision, inspection, traceability or compliance needs |
| Printing setup | Printer, nozzle, chamber, build plate, drying and annealing capability |
Frequently asked questions
Can I request a sample or trial quantity?
Trial quantities can be discussed according to product form and availability. Tell us what you need to prove during the trial, the intended process and the expected production quantity if the test succeeds.
Do you provide a data sheet or material documentation?
Available documentation depends on the selected material and supply route. List the documents required by engineering, purchasing or quality when you inquire so they can be checked before quotation.
Can the grade be selected from a product name alone?
No. Similar product names can cover different grades, colors, fillers and processes. Selection should be based on the finished application, environment and required property balance.
Can you supply custom dimensions or finished parts?
Custom sizes, blanks or finished parts can be reviewed where appropriate. A drawing with tolerances, quantity and material requirement is the best basis for quotation.
How should we evaluate an alternative to our current material?
Share the current grade, the part’s service conditions and the reason for changing it. A useful comparison looks at failure mode, processing, life, inspection and total project cost—not only a single property value.
What determines lead time?
Lead time depends on product form, grade, size, quantity, documentation, machining and current availability. Confirm the required delivery date and destination with the RFQ rather than assuming a standard schedule.
Send the drawing, application and quantity. We will use the project details to prepare a practical material and supply discussion.
Reviews
There are no reviews yet.