
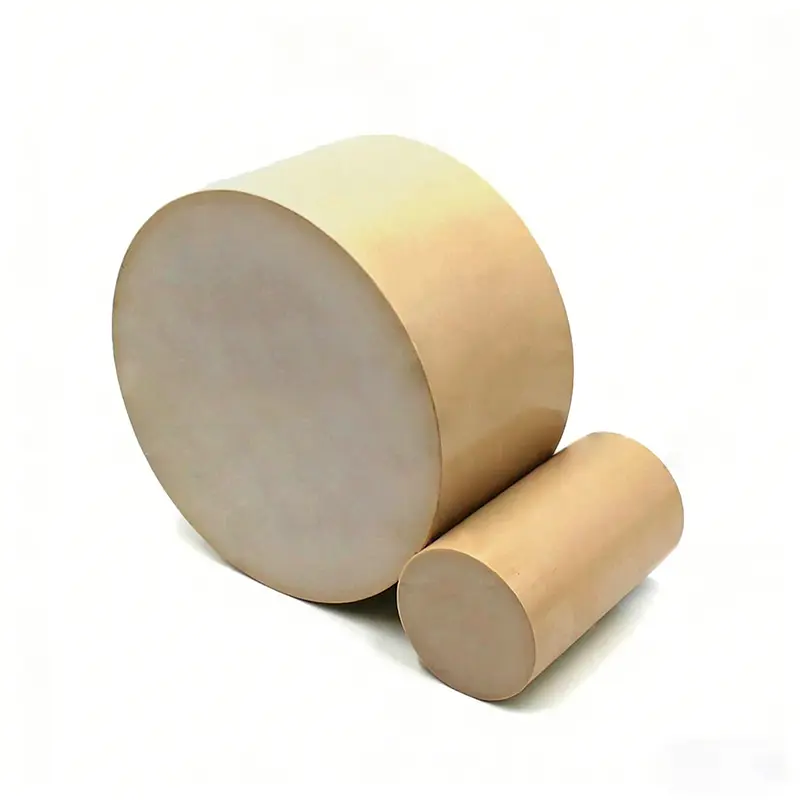
Aramid Fiber PEEK Rods
Precision-engineered Aramid Fiber-Filled PEEK Rods designed for demanding tribological applications. Thermally stress-relieved (annealed) to guarantee zero warpage and micro-inch dimensional stability during CNC machining. Ideal for non-abrasive, self-lubricating wear components mating against soft metals.
Need custom diameters or cut-to-length stock? Share your required dimensions, drawings, or quantity below for an immediate technical review and quotation.
Product information
Published information supports preliminary product selection. Confirm the exact grade, dimensions, tolerances, documentation and application suitability with the quotation for your order.
Description
Stress-Relieved Aramid Fiber Filled PEEK Rods are ultra-performance semi-finished engineering stocks designed for challenging dynamic wear and sliding applications. Formulated with a high-molecular-weight virgin Polyetheretherketone (PEEK) matrix and reinforced with high-tenacity aramid (Kevlar® style) synthetic fibers, this material offers an optimal balance of mechanical strength, self-lubrication, and mating-part protection.
Unlike conventional glass-reinforced or carbon-reinforced PEEK grades—which cause micro-scoring on softer counter-surfaces (such as aluminum, brass, or 316 stainless steel)—aramid fiber acts as a non-abrasive internal lubricant.
To guarantee zero internal distortion during machining, every stock rod undergoes a controlled multi-stage thermal annealing (stress-relief) cycle. This process neutralizes internal extrusion stresses, enabling high-speed CNC milling, deep drilling, and precision turning while maintaining micro-inch geometric stability and preventing stress cracking.
-
Glass Transition Temp (𝑇𝑔): 143℃ ( 289°F )
-
Melting Temperature (𝑇𝑚): 343℃( 649°F )
-
Continuous Operating Temp: Up to 250℃ ( 482°F )
How this product is normally specified
When specifying semi-finished Aramid PEEK rods, engineers should define stock dimensions based on finished component envelope geometry plus thermal/machining allowances, rather than raw resin parameters:
-
Dimensional Tolerances: Outer Diameter (OD) and Length specified according to standard ISO tolerance classes (e.g., ISO h9, h11, or custom machining oversized stock).
-
Thermal Expansion Allowance: Linear Coefficient of Thermal Expansion (CLTE) calculations to accommodate tight-tolerance bearing housing fits.
-
Thermal Stress State: Must be designated as “Fully Thermal Stress-Relieved / Annealed” for deep-hole drilling ( L/D >5 ) without core-cracking.
-
Surface Finish Baseline: Standard extruded profile vs. Precision Centerless Ground finish ( Ra < 0.8μm ).
-
Void-Free Quality: Homogeneous fiber distribution with zero internal porosity, verifiable via non-destructive testing (NDT).
Where this material can fit
This material is specifically specified for high-PV (Pressure-Velocity) environments where continuous sliding contact occurs against soft or unhardened counter-surfaces:
-
Automotive & Powertrain: Wear pads, high-temperature actuator bushings, and transmission thrust washers operating under hot oil immersion.
-
Fluid & Dynamic Seals: Non-scoring wear rings for centrifugal pumps, journal bearings, and unlubricated rotary vane valves.
-
Semiconductor Handling: Non-marking, low-particulate wafer handling tongs, vacuum chamber slide blocks, and low-friction wear components.
-
Chemical Processing: Metering rotors, valve seats, and process pump bearings subjected to aggressive solvents and high-pressure steam.
💡 Grade Upgrade Guide
If your current components made from 30% Carbon-Filled PEEK or Standard PTFE-Bearing Grades are causing premature shaft wear, scoring, or excessive running noise, Aramid Fiber Filled PEEK serves as the ultimate non-abrasive upgrade.
What to confirm before ordering
To help our technical team provide an accurate review and quotation, please share:
-
Detailed Component Drawings: 2D/3D CAD files specifying critical finish dimensions, GD&T, and required surface roughness (Ra).
-
Stock Size Requirements: Preferred rod diameter, wall thickness (if hollow), and cut-to-length dimensions.
-
Operating Environment Data:
-
Working Temperature Profile (Continuous vs. Peak)
-
Contact Pressure ( P ) & Sliding Velocity ( V ) → arget PV Value
-
Mating Surface Material & Hardness
-
-
Quality & Compliance Needs: Material Test Reports (MTC per EN 10204 3.1), RoHS, REACH, or Ultrasonic Test requirements.
-
Quantity & Delivery Schedule: Initial prototype volume and annual estimated usage (EAU).
Technical Property Data
| Propert | Test Method | Unit | Typical Range |
| Density | ISO 1183 | g/cm³ | 1.33 – 1.38 |
| Tensile Strength | ISO 527 | MPa | 105 – 125 |
| Flexural Modulus | ISO 178 | GPa | 5.0 – 6.5 |
| Izod Impact Strength, Notched | ISO 180/1A | kJ/m² | 5.5 – 8.0 |
| Deflection Temp under Load (HDT @ 1.8MPa) | ISO 75 | ℃ | 270-295 |
| Dynamic Coefficient of Friction | ISO 7148 / Tribometer | – | 0.18 – 0.25 |
| Specific Wear Rate | P = 1MPa, V = 1m/s | 10⁻⁶mm³/N·m | <0.9 |
Material overview
Understanding PEEK (Polyether Ether Ketone)
Why engineers use it
- Strong balance of heat, chemical and mechanical performance.
- Can be molded, extruded, machined or printed in suitable grades and equipment.
- Good fatigue and wear potential for demanding moving or loaded parts.
- Available in unfilled, glass-fiber, carbon-fiber and wear-modified grades.
- Suitable for precision components where long-term reliability justifies a specialty polymer.
Limits to consider
- High processing temperature requires capable equipment and controlled drying.
- Crystallinity, cooling and annealing can affect dimensions and performance.
- Reinforcement improves some properties but may reduce ductility or change machining behavior.
- Not every chemical, wear or medical application is covered by a standard industrial grade.
- PEEK can be unnecessary over-specification where PPS, PEI or another polymer meets the duty.
Grades and product forms
Unfilled PEEK provides the broad base-property balance. Glass-fiber grades generally target stiffness and dimensional control; carbon-fiber grades may add stiffness, strength and conductivity; bearing grades use fillers such as carbon, graphite or PTFE to tune friction and wear. Film, filament, powder, pellets and stock shapes each require different processing and purchasing information.
Performance points to review
| Evaluation area | Why it matters | Information to provide |
|---|---|---|
| Temperature behavior | Useful performance under elevated or changing temperature | Continuous and peak temperature, cycle length and time at load |
| Mechanical response | Strength and stiffness must match the real part geometry | Load direction, stress level, impact and fatigue expectations |
| Environmental resistance | Fluids, cleaning agents and atmosphere can change service life | Chemical name, concentration, temperature and exposure time |
| Dimensional control | Tight-tolerance parts depend on both material and processing | Finished dimensions, tolerances and assembly conditions |
| Electrical or insulation needs | Electrical requirements may influence grade and thickness | Voltage, dielectric, conductivity or insulation target |
These are engineering discussion points, not guaranteed property values. Final acceptance criteria should be agreed for the selected grade, process and order.
Typical application directions
These examples show where the material may be evaluated. They do not replace a suitability review for the finished component.
Fabrication and processing preparation
Share the finished part drawing as well as the requested rod diameter and length. This makes it possible to discuss machining allowance, tolerance, cut length, quantity and whether a closer starting size could reduce waste.
Where the application is critical, define what a successful trial looks like before material is ordered: dimensions after processing, visual condition, mechanical response, assembly fit or another measurable result.
When another material may be better
PPS, PEI, PSU/PPSU or a conventional engineering plastic may be more economical when temperature, chemical and mechanical requirements are moderate. PEEK is justified when several demanding requirements occur together or when service life and reliability outweigh raw-material cost.
We recommend sharing the current material and the reason it is being reconsidered. Cost, processability, supply form and inspection burden belong in the decision alongside technical performance.
Information needed for an accurate quotation
A useful RFQ reduces follow-up questions and helps us distinguish between a material request and a finished-part requirement.
| Product form | Raw material, stock shape, semi-finished blank or completed part |
|---|---|
| Dimensions | Nominal size, finished size and tolerances |
| Quantity | Trial quantity, first order and estimated annual demand |
| Application | Part function and current material, if any |
| Operating temperature | Continuous range, peak temperature and cycle duration |
| Environment | Chemicals, gases, moisture, pressure, vacuum or outdoor exposure |
| Mechanical duty | Load, speed, impact, wear and mating components |
| Documentation | Drawing revision, inspection, traceability or compliance needs |
Frequently asked questions
Can I request a sample or trial quantity?
Trial quantities can be discussed according to product form and availability. Tell us what you need to prove during the trial, the intended process and the expected production quantity if the test succeeds.
Do you provide a data sheet or material documentation?
Available documentation depends on the selected material and supply route. List the documents required by engineering, purchasing or quality when you inquire so they can be checked before quotation.
Can the grade be selected from a product name alone?
No. Similar product names can cover different grades, colors, fillers and processes. Selection should be based on the finished application, environment and required property balance.
Can you supply custom dimensions or finished parts?
Custom sizes, blanks or finished parts can be reviewed where appropriate. A drawing with tolerances, quantity and material requirement is the best basis for quotation.
How should we evaluate an alternative to our current material?
Share the current grade, the part’s service conditions and the reason for changing it. A useful comparison looks at failure mode, processing, life, inspection and total project cost—not only a single property value.
What determines lead time?
Lead time depends on product form, grade, size, quantity, documentation, machining and current availability. Confirm the required delivery date and destination with the RFQ rather than assuming a standard schedule.
Send the drawing, application and quantity. We will use the project details to prepare a practical material and supply discussion.
Reviews
There are no reviews yet.